


An OEM connector project often begins with a deceptively short message: “We need an RJ45 plug for this cable.” The real design space includes conductor layout, insulation diameter, cable outside diameter, contact geometry, shielding, strain relief, crimp tooling, packaging and production inspection.
The goal of an RJ45 OEM connector RFQ is not to predict every design decision. It is to make the unknowns visible and turn the first sample into a controlled learning step.
Stage 1: Define the cable before discussing the plug
The cable is the connector’s working environment. Provide:
- Category and target application.
- Solid or stranded conductor construction.
- Conductor diameter and insulation outside diameter.
- Core arrangement, separator or filler structure.
- Overall cable diameter and tolerance.
- Unshielded or shielded construction and drain-wire details.
- Jacket material and the intended termination environment.
When possible, provide actual cable samples from production, not only a nominal drawing. A plug that fits the nominal center may still be sensitive to normal cable variation.
Stage 2: Translate application needs into interfaces
Separate requirements into interfaces that can be reviewed:
| Interface | Questions to answer | Approval evidence |
|---|---|---|
| Wire entry | Do conductors enter in the correct order without damage? | Section view, insertion trial, repeated samples |
| Contacts | What geometry and plating requirement matches the application? | Drawing, material/plating inspection plan |
| Housing | Does latch, cavity and cable entry fit the mating and cable system? | Dimensions, mating check, visual sample |
| Shield | How is shield contact and strain relief maintained? | Assembly review and continuity check |
| Tooling | Which crimp tool, die and preparation method are approved? | Work instruction and terminated sample set |
| Packaging | How are parts counted, protected, labeled and traced? | Pack-out sample and label approval |
Stage 3: Choose a meaningful first sample
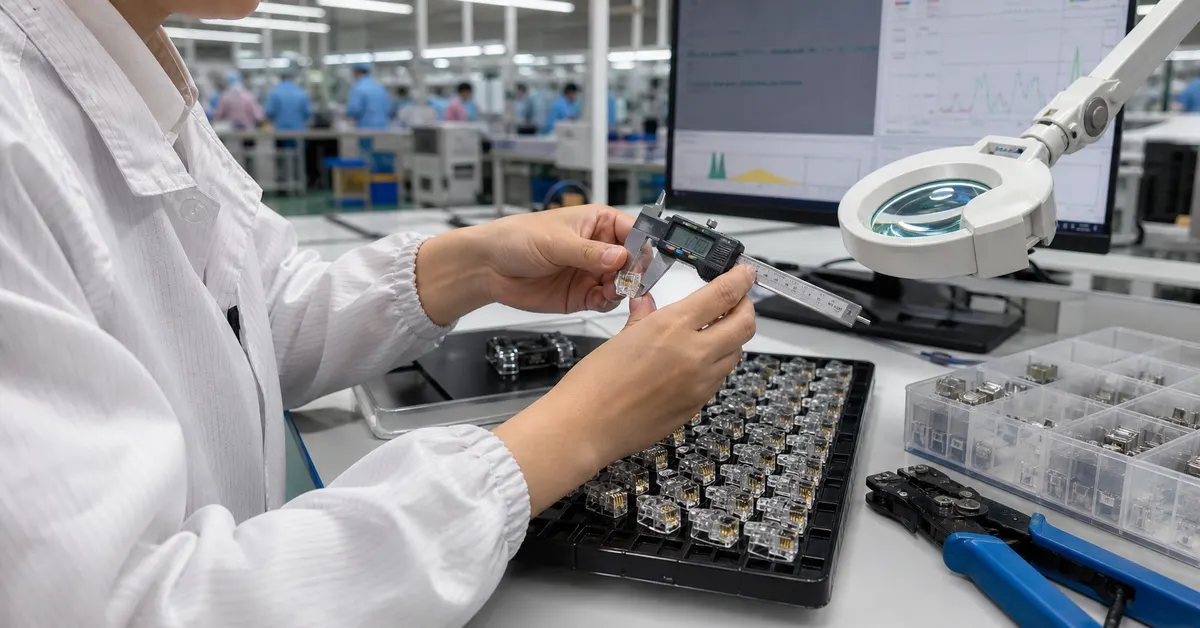
A meaningful sample represents the intended production system. Use the actual cable, specified connector parts and expected termination tool. Build several terminations across the agreed preparation range. Inspect conductor position, contact seating, shield contact, latch function, strain relief and appearance.
For termination equipment, review the tools and accessories category. For reference connector families, compare RJ45 modular plug constructions.
Stage 4: Build the approval matrix
Divide approval into four groups:
- Dimensional: critical fit dimensions and measurement method.
- Assembly: cable preparation, wire insertion, crimp or tool-free operation and visual criteria.
- Functional: mating, retention, continuity and the agreed network or electrical test configuration.
- Commercial: color, logo if authorized, labels, pack quantity, carton and documents.
Not every dimension needs the same control level. Identify the characteristics that truly affect cable fit, contact position, shield interface and mating. This keeps inspection focused on risk rather than paperwork volume.
Stage 5: Freeze the revision before volume release
Record the approved drawing, material choices, tooling version, work instruction, sample, test method and packaging artwork. Define which later changes require notification or re-approval. Without this baseline, a “small improvement” in one component can change another interface.
Why integrated manufacturing matters
RJ45 connector performance depends on interactions between molded geometry, stamped contacts, metal shielding and final assembly. DetwilerTech’s in-house mold design and manufacturing, precision metal stamping, injection molding, assembly and self-developed automation capabilities allow cross-functional issues to be reviewed within one project workflow. Inspection resources such as dimensional equipment, X-ray fluorescence thickness measurement and network test instruments can support agreed checks. The exact plan should still be defined for the application; equipment names alone are not a substitute for acceptance criteria.
RFQ attachment checklist
- Cable drawing and representative cable samples.
- Target connector layout and mating interface.
- Critical dimensions and tolerances.
- Shielding, contact and housing requirements.
- Approved termination method and tool.
- Expected annual and batch quantities.
- Logo, color, labels and packaging instructions.
- Sample quantity, test configuration and acceptance matrix.
- Revision-control and change-notification expectations.
Create a sample handoff record
When the sample leaves engineering, send it with a short controlled record. Identify the cable batch, connector revision, tooling, preparation length, operator or process, inspection date and test configuration. Mark whether the sample is for dimensional review, termination evaluation, functional testing or final appearance approval. This prevents one prototype from being treated as approved for purposes it was never built to answer.
Keep one approved reference sample on each side when practical. If production or packaging later changes, compare against the same baseline and document the reason. For distributors, the handoff record also helps sales and quality teams answer customer questions without reconstructing the entire development history from email.
Frequently asked questions
What should an RJ45 OEM RFQ include?
Include the target application, cable conductor and insulation dimensions, cable outside diameter, pin count and layout, shield requirement, housing and contact requirements, termination tooling, quantities, packaging and approval tests.
Why should more than one sample be terminated?
Multiple terminations reveal repeatability. A single good sample may not expose sensitivity to cable preparation, conductor insertion, crimp tooling, shield contact or normal dimensional variation.
When should tooling or packaging changes be frozen?
Freeze them after the representative sample and inspection plan are approved, but before volume release. Later changes should use documented revision control and a defined re-approval rule.
Prepare an OEM sample that answers the right questions
Explore DetwilerTech RJ45 connector families, then send your cable drawing, samples, target quantity and approval requirements. We can organize the first review around the cable-to-connector interfaces that carry the most risk.
CUSTOMER DISCUSSION
Article Discussion
Read questions and experience from other customers, then add your own product or project feedback.
No published comments yet. Start the first useful discussion.
Sign in to comment
Registered customers use their account display name and can track moderation status from the account page.
Customer Login Create an Account